

ไลน์ขึ้นรูปม้วนLinia CZS
Zeman




ข้อมูลพื้นฐาน
- ชื่อเครื่องจักร:
- ไลน์ขึ้นรูปม้วน
- ผู้ผลิต:
- Linia CZS
- รุ่น:
- Zeman
- ปีที่ผลิต:
- 2010
- สภาพ:
- เกือบใหม่ (ใช้แล้ว)
- ประสิทธิภาพการทำงาน:
- ทำงานได้เต็มประสิทธิภาพ
ราคาและสถานที่
- ที่ตั้ง:
- Mariusza Bojemskiego 9, 42-202 Częstochowa, Polska
รายละเอียดข้อเสนอ
- รหัสประกาศ:
- A21299532
- อัปเดต:
- อัปเดตล่าสุดเมื่อ 22.10.2569
คำอธิบาย
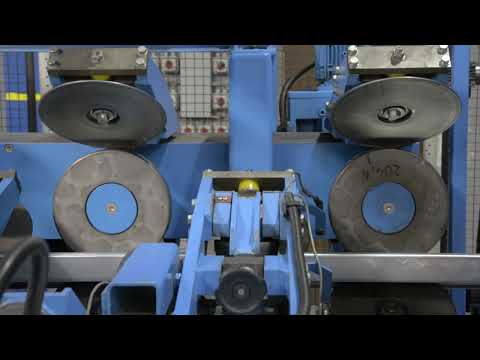
ZEMAN CZS LINE SPECIFICATIONS.
ZEMAN's flagship product, the fully automated "PURLIN" line, is used to produce open, cold-formed sections such as C, Z, and SIGMA, in various widths and shapes, thanks to fully automatic adjustment of the profiling rollers. Coils up to 750 mm wide and 1.25 mm to 3 mm thick sheet metal in grade S-390 and lower can be used as raw material. The machine is designed to produce components up to 15 m long. The width of the specially hardened profiling rollers is infinitely adjustable, using only dedicated software. A fully integrated "flying punching" device creates all types of mounting holes, and the entire process is continuous, meaning the material does not stop for individual operations such as punching holes or cross-cutting. To maintain production efficiency, the line speed is dynamically optimized. The machine decelerates and accelerates automatically without operator intervention.
A coil uncoiler with a maximum working load of 15 tons is mounted on a mobile trolley, enabling precise centering of the material strip before feeding it into the straightener.
The straightener, along with a crescent straightening system, allows for straightening the material, ensuring the required sheet flatness and reducing the crescent on the feed belt.
2. Punching Section
This section contains 5 double, "flying" punching portals, which can be equipped with 20 small (up to 40 mm) or 10 large (up to 100 mm) tools (punches and dies) for punching mounting holes.
A combination of these tools can also be used.
3. Pre-cutting Shear
A "flying" shear used to make preliminary holes for the cutting shear. This process is designed to maintain material continuity, resulting in a more precise profile shape, especially at its beginning and end. This is an adaptive guillotine that adjusts the width of the hole being cut to the width of the sheet metal strip.
4. Guide Carriage/SIGMA Modules
The guide carriage is used to center the sheet metal strip before entering the profiler. It is interchangeable
with the module for producing Sigma-shaped profiles. To produce S+ profiles,
the guide table should be removed and two Sigma modules inserted. These modules position
fully automatically and independently, left and right.
6. Rotary Cut-Off Guillotine.
The rotary cut-off guillotine with hook knives is used to finally cut the profile from the material strip
using the holes made by the pre-cutting guillotine. This is a "flying" guillotine,
so the sheet metal does not stop during the cutting process. Depending on the profile being produced, a properly oriented cutting cassette should be attached.
7. Receiving Table
The receiving table is used to automatically discharge the completed profiles from the roller conveyor. The elements are then manually arranged into a package. The design allows for easy bundling of the package. The table is designed to accept 15-meter profiles and allows for access by a forklift or overhead crane to collect the package of profiles.
Isdpfx Apsymampe Isii
ผู้จัดหา
ลงทะเบียนตั้งแต่: 2006
188 ประกาศออนไลน์

ส่งคำขอ
โทรศัพท์ & แฟกซ์


 เยอรมนี
GildemeisterCTX 200E


 Weilerswist
TEMAREDCar Flat 3518 für PKW bis 1.438 kg - Kippbar


 Beograd
GaspariniSlitter


 Vilalba
DemaqEvo 4.0


 Wellingborough
FICEP1203 DJB


 Winkelhaid
KeaserSM12


 Fevziçakmak
TFON MACHINE CO.Leveling Machine | TF-L 9016


 Bremen
MAZAKVTC-300 C II


 Ciriè
STAMSTAM-2000


 Staufenberg
DURMAAD-S 30175

ตราความน่าเชื่อถือ Machineseeker
ตรารับรองความน่าเชื่อถือคืออะไร?
Machineseeker รับรองตัวแทนจำหน่ายที่ได้รับการคัดเลือกด้วยตราแห่งความไว้วางใจ Machineseeker ก่อนการอนุมัติ จะมีการตรวจสอบอย่างเป็นมาตรฐานและครอบคลุมโดยพนักงานที่มีประสบการณ์ของ Machineseeker
เราตรวจสอบอะไร?

การตรวจสอบ
ใบอนุญาตประกอบธุรกิจหรือสำเนาทะเบียนการค้า
การตรวจสอบ
ที่อยู่ไปรษณีย์ของผู้ขาย
การตรวจสอบความถูกต้องของ
การเชื่อมต่อบัญชีธนาคาร
การตรวจสอบ
การติดต่อทางโทรศัพท์
ได้ของหมายเลขหลัก
ข้อมูลทางเศรษฐกิจ
ต้องไม่มีลักษณะเชิงลบ
ข้อร้องเรียนของผู้ซื้อ
อาจนำไปสู่การเพิกถอนตราสัญลักษณ์สิ่งนี้หมายความว่าอย่างไรสำหรับคุณในฐานะผู้ซื้อ?
ด้วยตรารับรองความน่าเชื่อถือ Machineseeker คุณในฐานะผู้ซื้อสามารถระบุผู้ค้าที่ยั่งยืนได้โดยไม่ต้องตรวจสอบเอง ซึ่งมีแนวโน้มสูงมากที่จะดำเนินธุรกิจด้วยความซื่อสัตย์และสุจริต
แน่นอนว่าในระหว่างกระบวนการซื้อ อาจเกิดความเห็นไม่ลงรอยกันได้ Machineseeker ไม่รับผิดชอบต่อการละเมิดกฎหมายโดยผู้ซื้อหรือผู้ขายที่ใช้งานอยู่บน Machineseeker